Mining operations often face complex water management challenges, including groundwater infiltration, heavy rainfall accumulation, and underground flooding risks. A reliable drainage solution is essential to maintain safe working conditions, protect mining equipment, and ensure continuous production. A Submersible Mining Pump is designed to operate in harsh mining environments where high flow capacity, strong durability, and stable performance are required.
This article explains how submersible mining pumps work, why they are important for mining applications, how to select the right equipment, and how advanced pump solutions from AOTE help mining companies overcome drainage challenges with efficient and dependable technology.
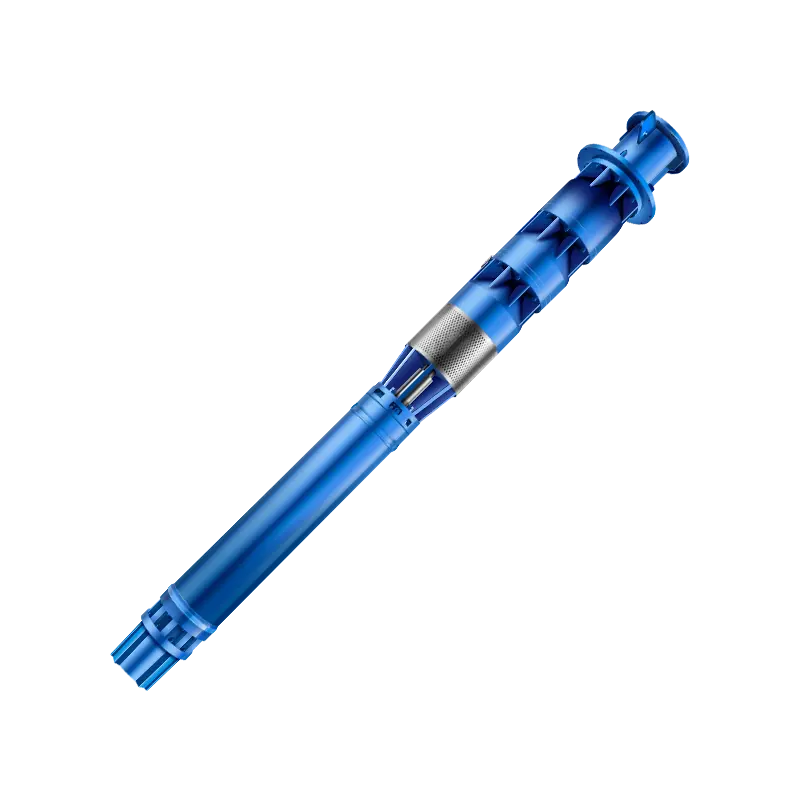
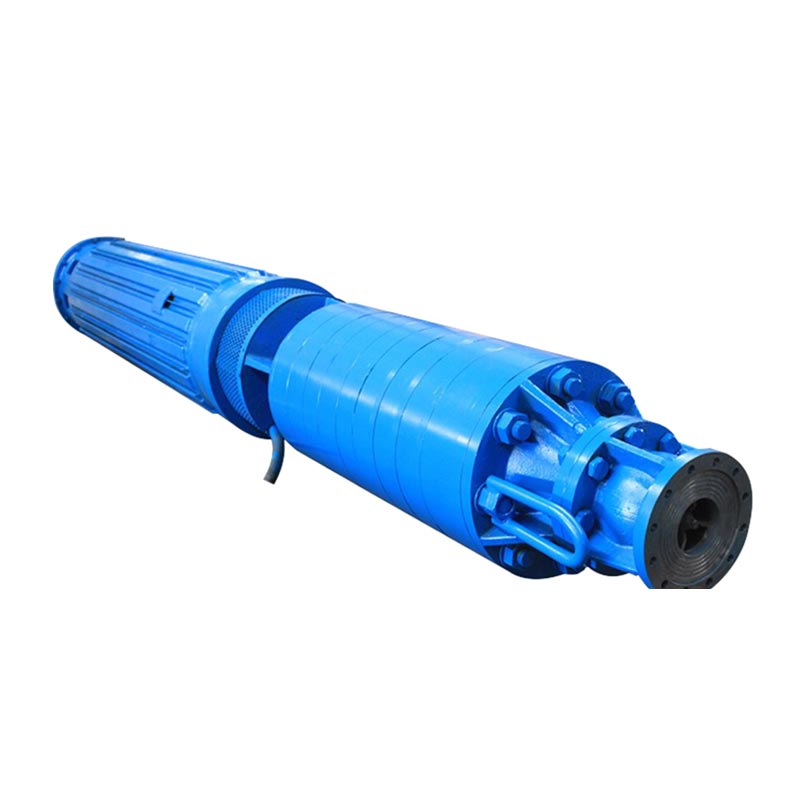
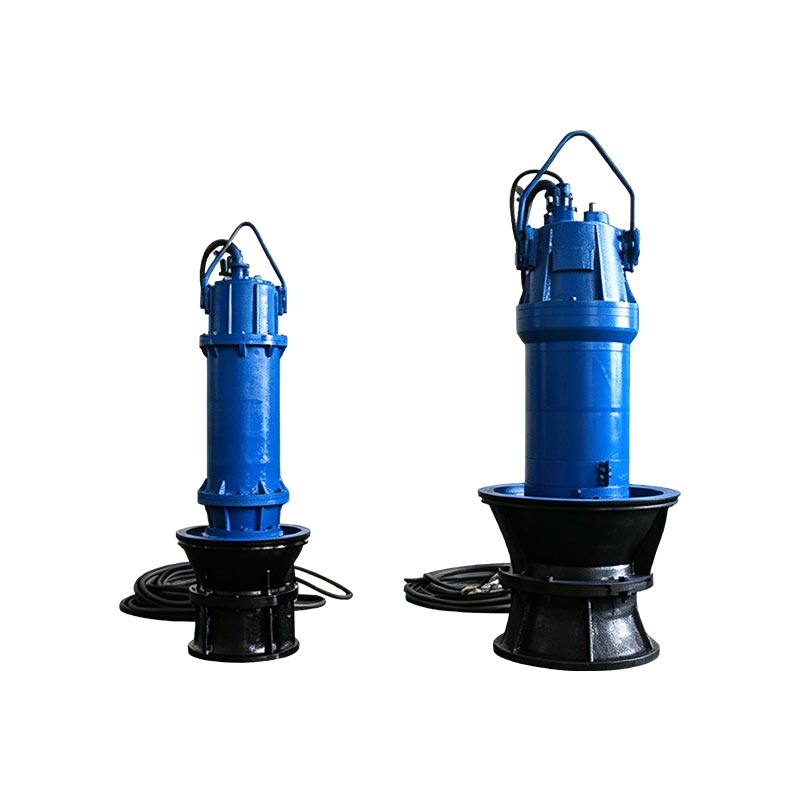
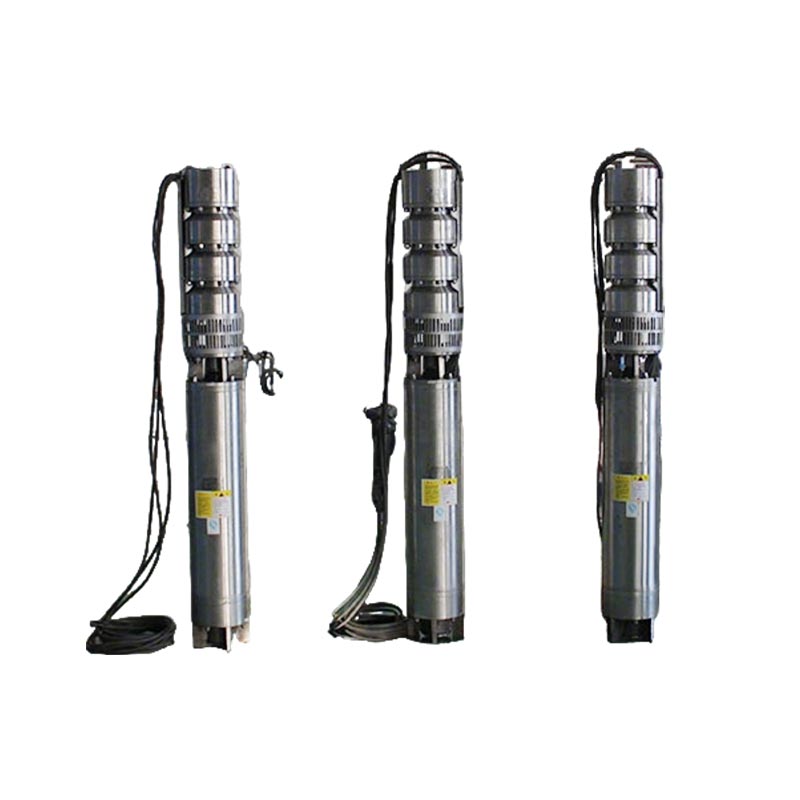
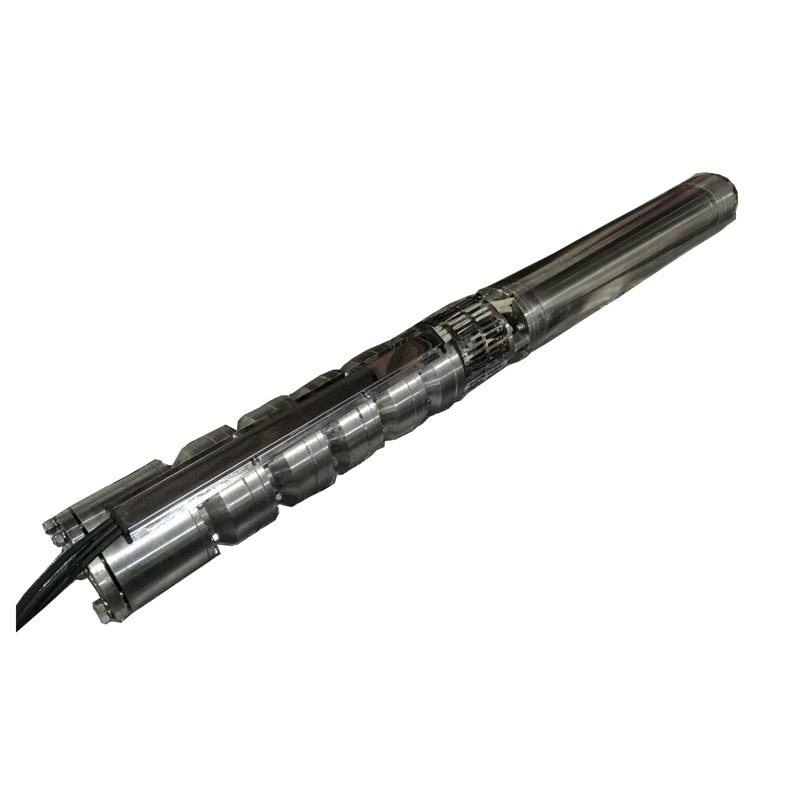
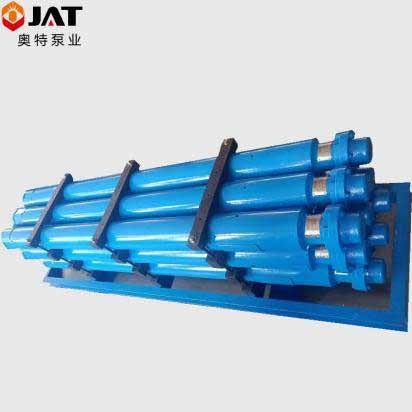
A Submersible Mining Pump is a specialized industrial pump designed to remove water from mining environments such as underground mines, open-pit mines, tunnels, and excavation areas. Unlike conventional surface-mounted pumps, submersible pumps are installed directly into the water source, allowing them to efficiently transfer large volumes of water while operating under demanding conditions.
Mining environments usually contain mud, sand, mineral particles, and corrosive substances. Therefore, mining pumps require stronger materials, enhanced sealing structures, and powerful motors to maintain reliable operation. A properly designed submersible mining pump can significantly reduce downtime caused by water accumulation and improve overall mine productivity.
AOTE specializes in the design and manufacturing of industrial submersible pumping equipment, including large submersible motor pumps and mining drainage solutions. The company focuses on providing stable pumping performance for industries that require continuous operation in challenging environments.
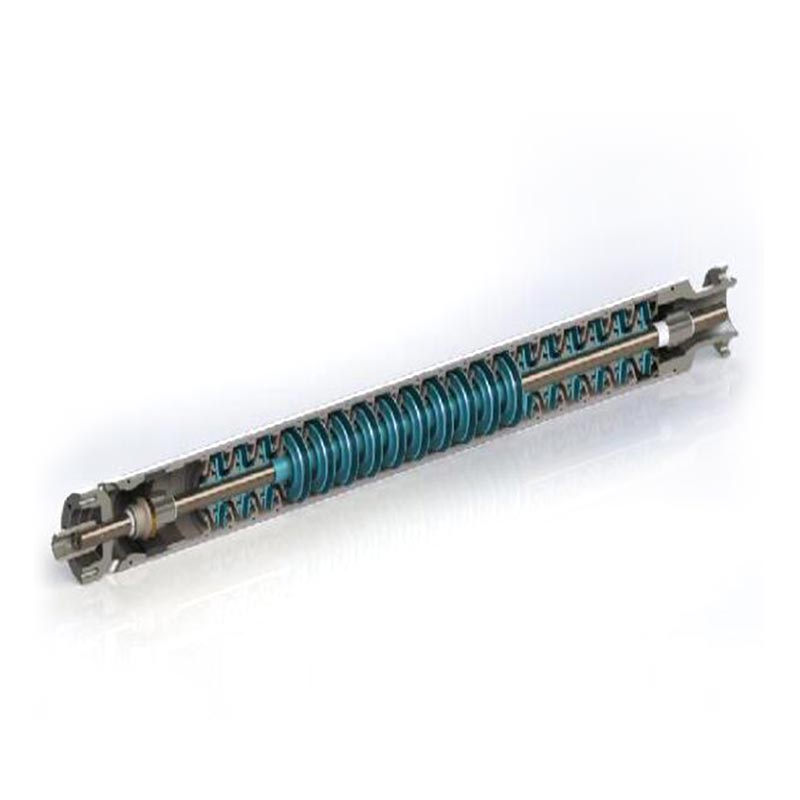
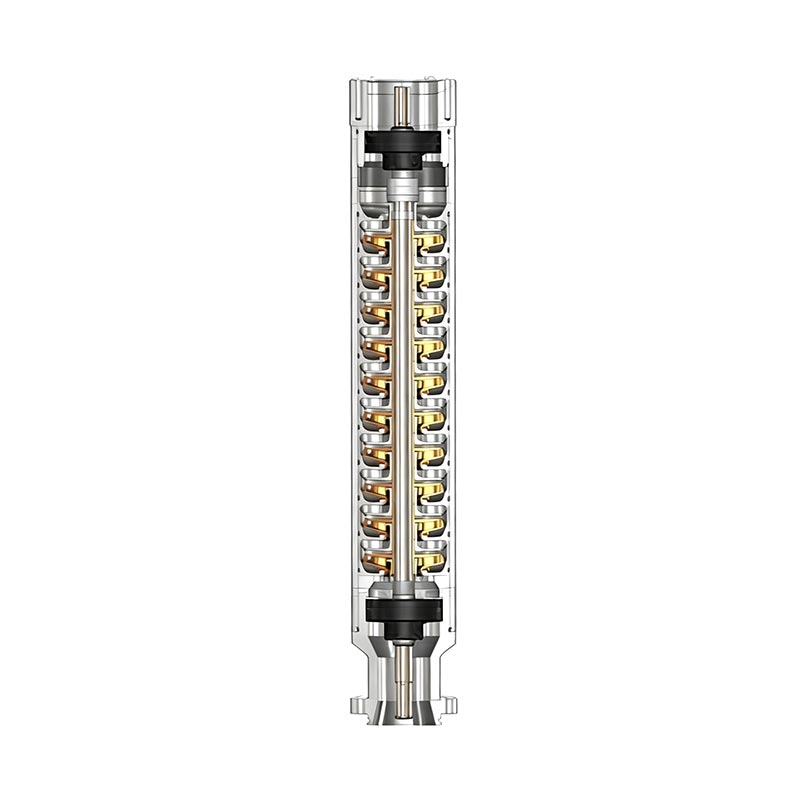
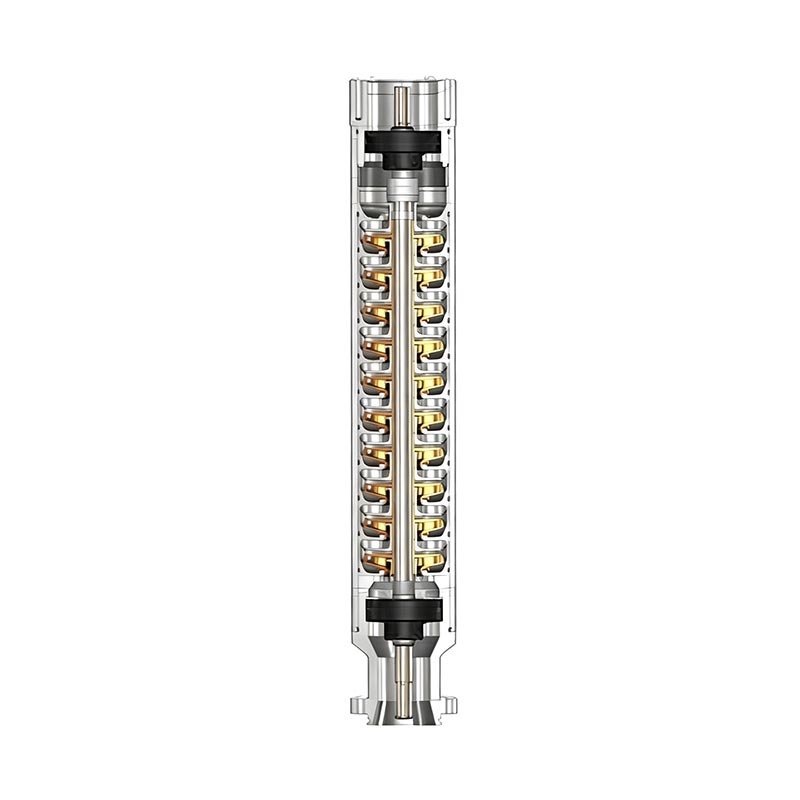
The working principle of a submersible mining pump is based on converting electrical energy into hydraulic energy. The motor drives an impeller system that creates centrifugal force, allowing water to enter the pump chamber and be pushed through the discharge pipeline.
Because the pump operates underwater, the surrounding liquid helps cool the motor during operation. This design reduces overheating risks and allows the equipment to run continuously for long periods.
| Component | Function |
|---|---|
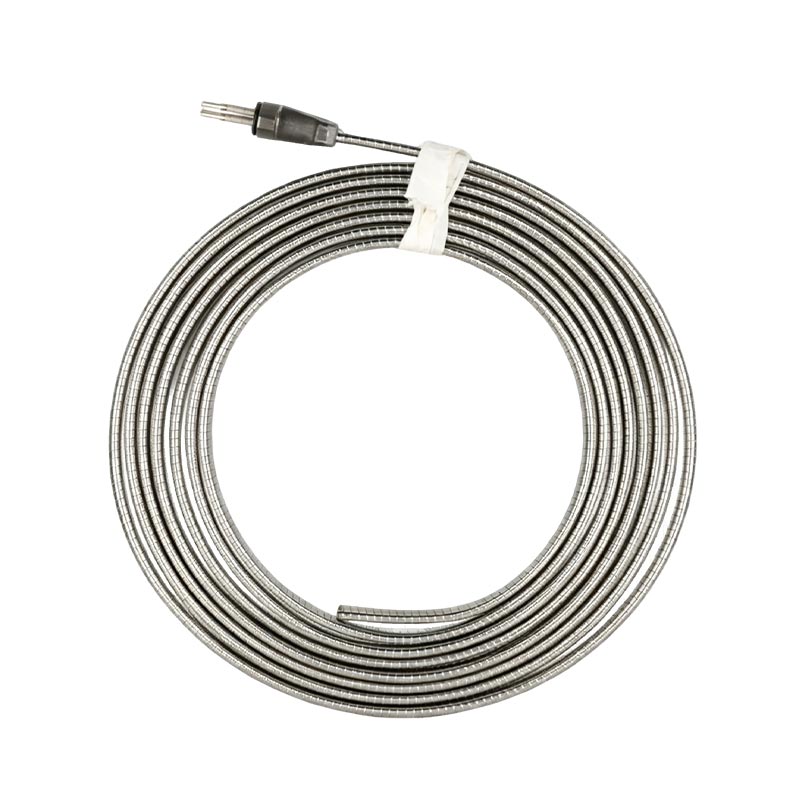
| Submersible Motor | Provides power to drive the pump assembly and maintain continuous operation. |
| Impeller | Creates centrifugal force to move water efficiently through the system. |
| Pump Casing | Protects internal components and withstands pressure from mining environments. |
| Mechanical Seal | Prevents water leakage into the motor section. |
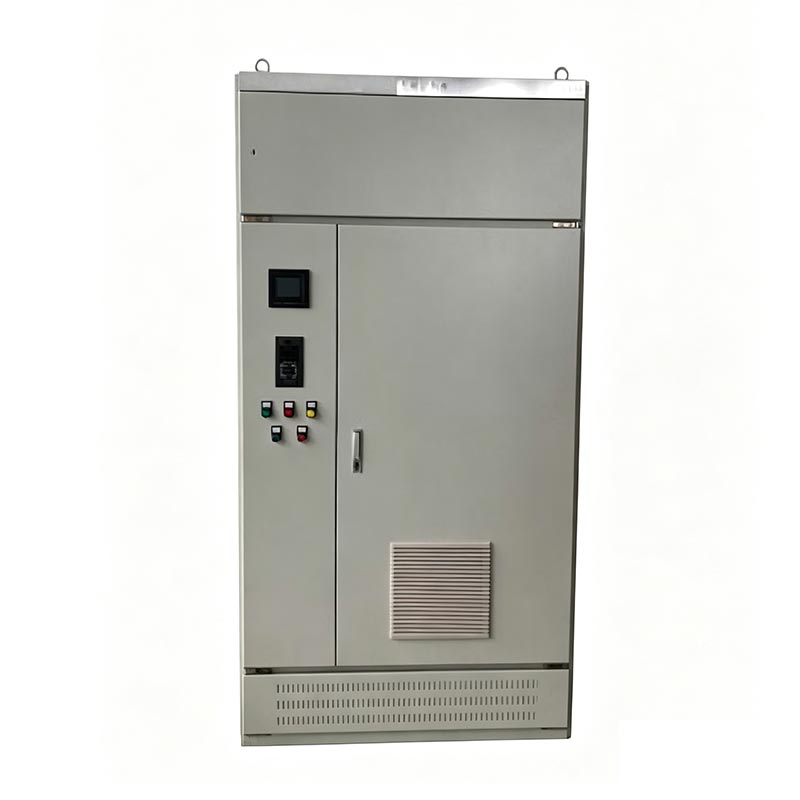
| Control System | Manages operation, protection, and monitoring functions. |
For deep mining applications, multi-stage designs can provide higher pressure and greater lifting capability, making them suitable for removing water from significant depths. Some mining pump models are developed with high-head performance to handle demanding drainage conditions.
Water management is one of the most critical challenges in mining. Excessive water can slow production, damage machinery, create safety hazards, and increase operational costs. A reliable drainage system helps maintain stable working conditions and protects valuable assets.
A submersible mining pump provides several advantages compared with traditional drainage equipment:
In mining projects, unexpected water problems can lead to expensive production interruptions. Selecting a suitable pumping system from the beginning helps companies maintain operational stability and reduce long-term costs.
Not every industrial pump can meet mining requirements. Mining applications require specialized designs that can withstand heavy-duty conditions.
| Feature | Importance in Mining Applications |
|---|---|
| High Wear Resistance | Protects pump components from damage caused by sand, minerals, and solid particles. |
| Strong Motor Performance | Ensures stable operation under continuous heavy loads. |
| Excellent Sealing System | Prevents water penetration and improves equipment reliability. |
| High Flow Capacity | Allows faster removal of mine water. |
| Flexible Installation Options | Supports different mining layouts and site conditions. |
Material selection is also important. Components must resist corrosion and mechanical wear caused by underground environments. High-quality cast materials and optimized hydraulic structures help improve pump efficiency and durability.
Selecting the correct pump requires evaluating several technical factors. Choosing equipment only based on purchase price may result in higher maintenance expenses and reduced operational efficiency.
Professional manufacturers can provide customized recommendations based on actual mining conditions. This approach helps companies avoid improper equipment selection and achieve better performance.
Submersible mining pumps are widely used in various mining and industrial environments.
Different applications require different pump specifications. Large-scale mining projects often need high-pressure and high-flow solutions, while smaller operations may require compact systems with flexible installation options.
AOTE focuses on developing reliable pumping solutions for industrial applications. With experience in submersible motors, electric submersible pumps, and large-scale pumping equipment, the company provides solutions designed for demanding environments.
The company’s product range includes mining-related submersible pump solutions, heavy-duty pumping systems, and customized equipment designed according to customer requirements. AOTE combines engineering experience with manufacturing capability to help customers improve drainage efficiency and operational reliability.
For mining companies, choosing the right equipment supplier is not only about purchasing a pump. It is about obtaining a complete solution that includes technical support, product reliability, and long-term service value.
Choosing and operating a Submersible Mining Pump requires a clear understanding of performance requirements, installation conditions, and maintenance practices. The following questions address common concerns from mining operators and industrial users.
A submersible mining pump is specifically engineered for demanding mining environments where water may contain mud, sand, minerals, and other solid particles. Compared with standard water pumps, mining pumps usually feature stronger wear-resistant components, more durable motors, improved sealing structures, and higher resistance to continuous operation.
Standard pumps are generally designed for clean water applications, while mining pumps must maintain stable performance under harsh working conditions. The specialized design allows mining pumps to provide reliable drainage even in underground and open-pit mining operations.
The operating life of a submersible mining pump depends on factors such as pump quality, working environment, water conditions, maintenance schedule, and operating load. High-quality mining pumps designed with durable materials can operate continuously for extended periods when properly installed and maintained.
Regular inspections, proper electrical protection, and timely replacement of worn components can significantly extend service life. A professional supplier such as AOTE can help customers select suitable pump specifications according to actual operating conditions.
Yes. Many mining submersible pumps are designed specifically to handle water containing suspended solids. Mining environments often involve sediment, mineral particles, and muddy water, which require pumps with strong wear resistance and optimized hydraulic designs.
Before selecting a pump, users should evaluate particle size, concentration, and water characteristics to ensure the selected equipment can provide efficient and stable operation.
Although submersible mining pumps are designed for durability, regular maintenance is still necessary to maintain performance. Recommended maintenance practices include:
A preventive maintenance plan helps reduce unexpected failures and improves the reliability of mining drainage systems.
The correct pump size depends on several factors, including required flow rate, pumping head, water conditions, operating hours, and installation environment.
| Selection Factor | Key Consideration |
|---|---|
| Flow Rate | Determines how quickly water can be removed from the mining area. |
| Total Head | Defines the pumping height and pressure requirements. |
| Water Characteristics | Affects material selection and wear resistance requirements. |
| Installation Space | Influences pump dimensions and configuration. |
| Power Availability | Ensures compatibility between the pump motor and site electrical system. |
Working with an experienced manufacturer allows mining companies to receive technical recommendations based on real application requirements instead of selecting equipment only by general specifications.
As mining operations become more efficient and environmentally responsible, pumping technology continues to develop. Modern mining companies require equipment that provides higher efficiency, lower energy consumption, and improved reliability.
Future submersible mining pump systems are expected to focus on several important improvements:
Manufacturers that continue investing in research and engineering improvements can provide more effective solutions for modern mining challenges. AOTE continues to focus on industrial pumping technology to support customers requiring dependable water management systems.
Water management plays a vital role in maintaining safe and efficient mining operations. A dependable Submersible Mining Pump provides an effective solution for removing underground water, handling challenging conditions, and reducing production interruptions.
The right pump selection requires careful consideration of flow requirements, pumping depth, water characteristics, and operating environment. Investing in suitable equipment not only improves drainage performance but also reduces maintenance costs and enhances operational stability.
With professional manufacturing capabilities and industrial pumping experience, AOTE provides reliable submersible mining pump solutions designed to meet the needs of demanding applications. Whether for underground mines, open-pit projects, or industrial drainage systems, choosing a properly engineered pumping solution can make a significant difference in long-term performance.
AOTE is committed to providing durable and efficient submersible mining pump solutions for customers worldwide. If you need a reliable pumping system designed for challenging mining conditions, contact us today to discuss your requirements and receive professional support for your project.